
Heavy Equipment Operator Training: 7 Proven Steps to Safer Sites
Heavy equipment operator training on African construction sites works best as a seven-step system: a competence baseline, the right certification route, machine-based practice, a daily inspection, habit coaching, strict site rules, and ongoing measurement. Operator habits drive fuel use and undercarriage wear, and breakdowns, so the cab is the cheapest place to protect a machine. Running an engine 200 to 300 rpm lower can cut fuel use by approximately 10%, while a skipped walk-around can end a shift with a failed machine or an injured worker.
Technical Snapshot: Core Training Specifications
| Parameter | Detail |
| Primary Topic | Heavy equipment operator training and daily inspection on African sites |
| Core Training Stack | Classroom, simulator, workshop, and supervised live-machine practice |
| Certification Routes Covered | Kenya, South Africa, Nigeria, Ghana, and OEM tiers (Caterpillar Levels I to III) |
| Inspection Frequency | Every shift, before start-up, with operator tag-out authority |
| Biggest Controllable Cost Lever | Engine speed discipline: operating at 200 to 300 rpm reduces fuel use by approximately 10%. |
| Binding Constraint | Accredited training capacity, because plant training needs a working fleet, fuel, a workshop, and open ground |
| Fastest Levers | Pre-start walk-around, work-mode discipline, travel-time limits, and exclusion zones |
| Benchmark Metric | Caterpillar Level III pass marks: 100% on the safety quiz, 80% on the written test, five years of experience |
| Ownership Shift | Dealer-run academies, with Ganatra targeting 5,000 certified East African operators by 2029 |
Heavy equipment operator training pays off through lower fuel burn, longer component life, and fewer incidents, making it as much a maintenance strategy as a safety duty. Contractors that treat the operator as the first technician protect both their people and their fleet value.
Introduction: Heavy Equipment Operator Training
Heavy equipment operator training decides how long a machine lasts before a technician ever touches it. A 20-tonne excavator in skilled hands burns less fuel, wears its tracks more slowly, and reports faults early. In untrained hands, the same machine loses money through idle hours, abused undercarriages, and avoidable breakdowns. This article covers the operator side of the fleet, while the complete equipment maintenance guide covers technician-level servicing.
Demand for certified operators already exceeds supply. Training providers such as Ganatra’s regional training push describe fleets expanding faster than the accredited capacity to staff them, and plant training remains expensive because it requires a working fleet, fuel, a workshop, and open ground. Contractors fill the gap with uncertified labour, and the cost lands on safety records, machine life, and project timelines.
A sound heavy equipment operator training programme in Africa, therefore, does more than teach controls. Screening comes first, followed by certification against a recognised standard, machine-specific practice, a daily inspection, habit coaching, strict site rules, and measurement. Those seven steps are listed below, and each one ties equipment operator safety to fleet availability.
The Seven Steps at a Glance
The programme works in sequence because each step depends on the one before it. Certification means little without a baseline, and a checklist achieves little when operators never learn why each item matters. The table below names the owner of each step and the cost or risk it controls, so a site manager can assign responsibility before the first operator starts.
Heavy Equipment Operator Training: Seven Steps, Owners and Targets
| Step | Focus | Owner | Cost- or Risk-Controlled |
| 1 | Competence baseline | Site manager and HR | Unqualified operators on live machines |
| 2 | Certification route | Training manager | Legal exposure and unverified skill |
| 3 | Machine-based training | Dealer or in-house instructor | Costly early mistakes and rework |
| 4 | Daily inspection | Operator and supervisor | Breakdowns found late |
| 5 | Habit coaching | Supervisor and fleet manager | Fuel burn and component wear |
| 6 | Site safety rules | HSE officer | Struck-by incidents |
| 7 | Measurement and retention | Fleet manager | Skill decay and operator turnover |
Step 1: Set the Competence Baseline
Competence starts before training does. A site that screens candidates and authorises each operator by machine class removes the largest avoidable risk, an untested person on a 20-tonne machine. This step answers the question of what training an operator needs, then covers screening and machine-by-machine authorisation.
What Training Does a Heavy Equipment Operator Need?
An operator needs classroom instruction in safety and machine controls, supervised practical time on the specific machine class, and a documented competence assessment before working unsupervised. Most African markets add a recognised certificate, such as a trade test or an occupational certificate, and many employers add an OEM tier on top.
Screen Candidates Before the First Hour in the Cab
Screening filters out poor fits cheaply. Dangote’s heavy earth-moving machinery operator programme shows the model: it combines behavioural screening, safety training, classroom instruction, simulation, workshops, and field practice over a six-month period. Applicants need five WAEC or NECO credits, including English and Mathematics, or a national technical certificate with NABTEB or Trade Test passes, and the intake caps age between 22 and 35.
Authorise Each Operator Machine by Machine
Kenya’s occupational safety and health law sets a clear legal baseline. Section 6 makes training and supervision a duty of the occupier, and Section 55 allows the plant to run only for the work its designer intended and only under the supervision of a competent person. The Act defines a person as someone with adequate training, relevant qualifications, and experience.
Section 65 goes further for lifting machines. Only operators holding a written certificate from a recognised institution may operate them; trainees may work only under direct supervision; and no one under 18 may operate them. A written authorisation per machine class, signed by a supervisor, turns that duty into a site record.
Step 2: Choose the Right Certification Route
Heavy equipment operator certification proves a standard, and the standard differs by market. Governments run trade-test systems, qualification bodies register occupational certificates, and manufacturers run their own tiers. This step compares the government and qualification routes, tabulates them by country, and then explains where OEM and employer programmes fit.
Government Trade Tests and Registered Qualifications
Kenya’s National Industrial Training Authority (NITA) runs government trade testing for Artisan Grades I to III and encourages trainees to book a test during or after a course. That link ties a training certificate to a national standard rather than a provider’s own.
South Africa tests operators against registered occupational qualifications, and its legislation requires them to complete training and pass a competence assessment before operating an excavator. The excavator operator’s occupational certificate concludes with an external assessment of start-of-shift checks, machine operation, and safe working practices. SAQA lists it as past its registration end date, so confirm the current QCTO curriculum before enrolling staff.
Nigeria builds on national technical certificates, NABTEB passes, and Trade Tests I to III, and agencies layer short programmes on top. The training of 50 certified crane operators shows the pattern: a Level I and II course covering lifting procedures, equipment inspection, signalling, hazard identification, and risk assessment, with every trainee completing it.
In Ghana, the national heavy-duty operators association and a maritime university trained 50 operators from West and Central Africa, and six women broke into Ghana’s heavy machinery sector by completing the course. The association also plans a biometric authorisation system that would tie machine use to a certified operator’s identity.
Operator Certification Routes by Market
| Market | Route | Access point | Stated length or cycle |
| Kenya | Government trade test, Artisan Grades I to III | Booking through the National Industrial Training Authority | Three series a year (April, August, and December) |
| Kenya | Dealer Academy Plant Operator Course | Open enrolment, simulator-led | Four weeks, with accelerated modules |
| South Africa | Occupational certificate, excavator operator (NQF Level 3) | Accredited provider plus workplace experience | 75 credits plus external assessment |
| Nigeria | Trade Tests I to III, NABTEB, and employer programmes | Technical certificate or WAEC/NECO credits | Six months (employer programme); four weeks (crane Levels I and II) |
| Ghana | Association-led mobile crane and forklift course | Trainees from West and Central Africa | 10 weeks |
| OEM tiers | Caterpillar Levels I to III | Level I: under 3 years’ experience; Level II: 3 years or more; Level III: 5 years or more | Machine-family courses |
OEM and Employer Programmes
OEM tiers prove machine-specific skill. Caterpillar’s instructor-led operator training starts with Level I for entry-level operators and moves to Level II for operators with three or more years on a machine family. Level III is an assessment, not a course: it requires five years of operating experience and a Level II pass, and it is scored on the walk-around inspection, a safety quiz at 100%, and a written test at 80%.
Contractors should demand both layers of heavy equipment operator certification. A government or qualification body certificate demonstrates a recognised standard, while an OEM tier demonstrates that the operator can operate the fleet’s actual machines. Employers that run their own academies, as Dangote does, close the gap between the two by testing on the machines that earn money.
Step 3: Train on the Machine, Not Just in the Classroom
Classroom heavy equipment operator training alone does not make an operator productive on a live machine. This step covers the sequence that moves a trainee from software to steel, the supervised practice that follows, and the expected training duration.
Simulator-First Progression
Ganatra’s training institute fixes the order of instruction for every route: classroom first, then simulator, then workshop, then a live excavator. Its general manager argues that a trainee’s first hours on a real machine are the most expensive and most dangerous of the course, and that a simulator lets students make those mistakes in software. The institute describes its simulator as the only one of its kind in Africa, a claim that rests on the company’s own statement.
Supervised On-the-Job Practice
Simulator hours do not replace supervised site time. A foreman or trainer should run a structured on-the-job programme with documented task sign-offs, and manufacturers’ recommendations should shape what each machine class covers. Dealer-led courses deliver this on the customer’s jobsite with the customer’s machines, although they tie training to one brand’s service network, a trade-off that the comparison of OEM versus third-party servicing examines.
How Long Does Heavy Equipment Operator Training Take?
A heavy equipment operator training programme in Africa runs from four weeks to six months at the entry level. Ganatra’s plant operator course lasts four weeks and focuses on the excavator and backhoe loader; a 10-week course trains mobile crane and forklift operators in Ghana, and Dangote’s earth-moving programme runs for six months. Experienced operators then need 5 years before attempting a Caterpillar Level III.
Step 4: Enforce the Daily Operator Inspection
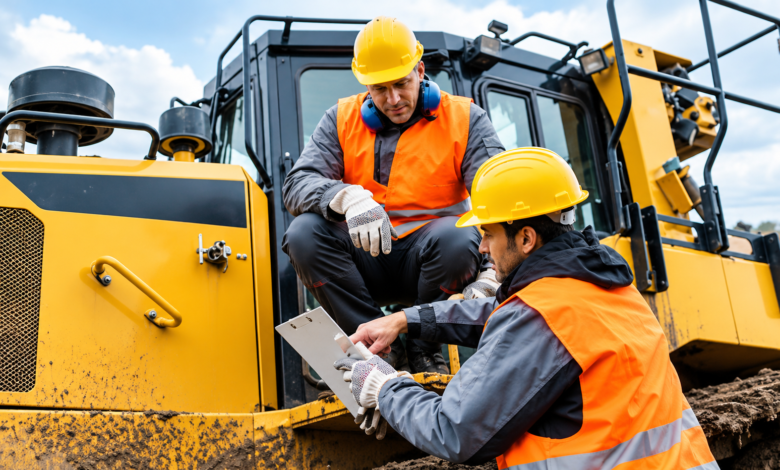
A daily inspection turns every operator into the first technician on the machine. This step covers the walk-around, in-cab functional checks, and the authority to tag a machine out, and concludes with a daily heavy equipment inspection checklist tailored for an equipment.
The 360-Degree Walk-Around
Operators start at the ground, because fresh drips reveal a leak before any gauge does. Boom, arm, and bucket welds and pins come next, then track tension, rollers, guards, and covers. Walking the same route in the same direction every shift teaches the eye what normal looks like, so a new weep or a loose bolt stands out.
In-Cab and Functional Checks
Seat, seatbelt, mirrors, and cameras come before the key turns. Once the engine runs, the operator tests the horn, lights, and reversing alarm, then cycles the controls and brakes at low speed to check for lag, noise, or drift. Every machine should carry a fire extinguisher and its operator’s manual, and the operator should confirm that both are present.
Tag-Out Authority and Records
An inspection only works if the operator can stop the machine. Give every operator written authority to tag out a machine with a critical defect, such as a cracked weld, a failed brake, or a leaking hydraulic hose, and require a supervisor’s signature before the tag is removed. Sort other defects into same-shift and scheduled repairs, and log them so the workshop can see patterns. That discipline moves a fleet toward preventive rather than reactive maintenance.
Further Reading: Preventive vs Reactive Maintenance in Construction: 5 Proven Savings
Heavy Equipment Daily Inspection Checklist for Excavators
| Check | What the operator looks for | Failure it prevents |
| Ground beneath the machine | Fresh oil, fuel or coolant drips | Hydraulic or engine failure from slow leaks |
| Boom, arm and bucket welds and pins | Cracks, missing pins, excess play | Structural failure and dropped loads |
| Track tension and rollers | Sag outside manual limits, packed debris, seized rollers | Bushing and sprocket wear (loose), undercarriage stress (tight), scrubbed tracks (seized) |
| Fluid levels | Engine oil, hydraulic oil, coolant, and fuel | Starvation, overheating, and condensation in the fuel tank |
| Guards, covers, ROPS, and seatbelts | Missing, bent, or damaged parts | Entanglement and rollover injuries |
| Lights, horn, reversing alarm, mirrors, cameras | Working order and clean lenses | Struck-by incidents in blind spots |
| Controls and brakes | Lag, noise, or drift at low speed | Loss of control on slopes |
| Extinguisher and manual | Present and in date | Fire escalation and wrong-procedure errors |
Step 5: Coach Habits That Extend Machine Life
Operators control the three largest wear drivers on a machine: engine speed, travel, and handling. This step explains how operator behaviour affects equipment life, then covers engine speed, travel time, and loader handling, and concludes with a table that maps each habit to the component it damages.
How Does Operator Behaviour Affect Equipment Life?
Operator behaviour sets how hard a machine works for each tonne it moves. Aggressive throttle use, long travel, hard direction changes, and wheel spin increase fuel consumption and accelerate wear on engines, undercarriages, brakes, and tyres. Smooth, planned movements lower both, so two operators on the same machine can produce very different service lives and breakdown rates.
Manufacturers accept this. Volvo CE expects advanced control systems to improve productivity and reduce reliance on operator skill over time, yet its own wheel loader study found productivity up to 700% higher and fuel efficiency up to 200% better for professional operators than for novices. Treat those figures as upper bounds from one OEM study, not as fleet averages.
Engine Speed and Work Modes
Engine speed is the cheapest habit to coach. Volvo CE advises that running 200 to 300 rpm lower can cut fuel use by approximately 10%, and operator training to cut costs rests on that kind of discipline. Supervisors should teach operators to match the work mode to the task and to avoid idling during breaks.
Volvo’s excavator fleet manager guidance adds two claims. Operators who default to the highest work mode regardless of task can cost an owner upwards of USD 10,000 per excavator per year, and excessive travel time is the main cause of undercarriage wear.
Travel Time and Undercarriage Wear
Travel is the habit that quietly consumes tracks. Coach operators to dig from one position as long as the work face allows, to bring haul trucks to the machine instead of walking the machine to the truck, and to avoid steep climbs and sharp turns. Check track tension weekly against the manual, because loose and overtight settings both shorten undercarriage life. Undercarriage failures stop the machine, and the downtime costs a fleet far more than the parts bill. Every travel hour removed protects both availability and components.
Loader Handling and Tyres
Wheel loaders add tyre and brake wear to the list, and the cure is technique rather than parts. Coach gear selection that matches ground conditions, tyre pressures held to specification, and controlled direction changes. The table below maps every habit to the component it damages.
Operator Habit versus Wear Mechanism
| Habit | Component hit | Cost consequence |
| Highest work mode on every task | Engine and hydraulic pumps | Extra fuel burn without extra output |
| Long, unplanned travel | Tracks, sprockets, and rollers | Faster undercarriage wear and earlier rebuild |
| Ignoring track tension | Bushings, sprockets, and links | Premature replacement |
| Wheel spin on slick ground | Tyres | Shorter tread life and tyre downtime |
| Running low on tyre pressure | Tyres and fuel system | Higher fuel use and faster wear |
| Fuelling late or leaving tanks part full | Fuel tank and fuel system | Condensation, contamination, and costly repairs |
Step 6: Apply Site Safety Rules Without Exceptions
Construction site equipment safety rules protect the people around a machine as much as the operator inside it. This step covers exclusion zones and traffic plans, the banksman role, and blind spots by machine and attachment, then sets out the rules in a table that a site induction can adopt.
Exclusion Zones and Traffic Plans
In US data, job-site strike-by incidents account for nearly 20% of construction fatalities, and most of those involve heavy equipment and trucks. Equipment operator safety, therefore, depends on keeping people out of the machine’s working envelope.
Plants and pedestrians should never share a route. The UK government’s guidance on plant and person interface risks calls for physical barriers between pedestrian and plant routes, early visibility of oncoming plant, and an exclusion zone around working machines.
Queensland’s regulator, reviewing a worker struck by a vehicle in 2024, restates what an effective exclusion zone includes: signage, advance communication to workers, and engineering controls in high-risk areas.
Banksman and Communication
Every reversing or blind-side movement needs a designated banksman, and one agreed signal system, either hand signals or two-way radio. The banksman never stands in a blind spot, stops the machine on any loss of contact, and controls vehicles within the work area. Only one person signals at a time.
Tipper operators face extra rules on tipping position and on travelling with the body raised, and the new tipper truck maintenance tips cover the servicing side of the same fleet.
Blind Spots by Machine and Attachment
Blind spots vary by model, attachment, and load, and larger machines hide more ground. Operators know their own, but workers on the ground often do not, so every worker should learn the safe zone and the no-go zone for each machine on site. Mark the swing radius of excavators and the rear blind zone of loaders and tippers on the site plan.
Site Safety Rules for Heavy Equipment
| Rule | Enforced by | Stop-work trigger |
| No pedestrians inside the exclusion zone while plant works | Banksman and supervisor | Anyone who enters the zone |
| One bankman per machine and one signal system | Site supervisor | Signaller out of sight or radio contact lost |
| Seatbelt fastened and three points of contact when boarding | Operator, with HSE spot checks | The belt is unfastened in the cab |
| Plant and pedestrian routes kept separate | HSE officer | Routes cross without a barrier or marshal |
| Authorisation card held for the machine class | Supervisor | The operator lacks a card for that machine |
| Defect tags honoured | Supervisor | The tagged machine found running |
Step 7: Measure, Refresh, and Retain Operators
Heavy equipment operator training decays without measurement. This step covers the data that shows whether habits changed, the refresher cycles that keep skills current, and the records and retention practices that protect the training investment.
Telematics and Operator Scorecards
Telematics turns habits into numbers. Track idle share, hours in the highest work mode, travel hours, fuel per engine hour, and inspection completion for each operator, then review the figures monthly with the operator rather than only with management. Volvo CE says its monthly reports on travel time and work-mode use make training needs easy to spot, and the same logic works on any telematics platform.
Refresher Cycles
Schedule refreshers around events and calendars: a new machine or attachment, an incident or near miss, a poor scorecard, and an annual review. Manufacturer tiers give operators a ladder to climb, and a visible ladder gives them a reason to stay.
Records and Retention
Certified operators attract offers, so a documented ladder of pay and recognition protects the investment. Keep training records, authorisation cards, and inspection logs together for each operator, and schedule statutory plant examinations with an approved person. Kenya’s occupational safety directorate publishes qualifications for approved competent persons, including plant examiners. When a machine changes hands, the operator log doubles as its service history, which feeds the used tipper inspection checklist that buyers should apply.
Further Reading: Used Chinese Tipper Truck Maintenance Checklist: 9 Valuable Steps
Technical Block: Operator Economics of Fuel, Wear, and Inspection
Three calculations show why heavy equipment operator training pays: the fuel saved by engine-speed discipline, the reduced wear from shorter travel, and the cost of an inspection compared with the cost of a breakdown. Each uses illustrative inputs that readers should replace with their own fleet data.
1. Fuel Arithmetic of Engine Speed Discipline
A 20-tonne excavator burning 20 litres per hour for 2,000 hours uses 40,000 litres a year. Volvo CE’s figure of approximately 10% fuel saving at 200 to 300 rpm lower removes 4,000 litres per machine. At an assumed USD 1.40 per litre, that saves USD 5,600 per machine per year before any wear benefit is considered.
Illustrative Annual Fuel Saving from Engine Speed Discipline
| Fleet size | Annual fuel burn (litres) | 10% saving (litres) | Value at USD 1.40 per litre |
| 1 machine | 40,000 | 4,000 | USD 5,600 |
| 5 machines | 200,000 | 20,000 | USD 28,000 |
| 10 machines | 400,000 | 40,000 | USD 56,000 |
Replace the burn rate with the OEM figure for each model, and the pump price with the current local diesel price.
2. Undercarriage Wear Exposure and Parts Demand
How operator behaviour affects equipment life is most clearly seen in the undercarriage, because wear correlates with the hours spent travelling under load. If travel takes 30% of a 2,000-hour year, the tracks carry 600 hours of travel exposure. Coaching that cuts travel to 20% leaves 400 hours, a one-third reduction. Wear does not scale perfectly with hours, but the direction holds, and every hour removed delays the rebuild and eases the pressure that long lead times put on sourcing spare parts in Africa.
3. Cost of a Daily Inspection Against an Unplanned Breakdown
A 15-minute walk-around across 250 working days costs 62.5 operator-hours per year. At an assumed loaded operator cost of USD 4 per hour, the total is USD 250. A five-day stoppage of a machine earning USD 60 per hour over eight-hour days costs USD 2,400 in lost output, approximately 10 times the annual inspection cost. One avoided a breakdown, therefore repaying the routine for the year.
Conclusion: Operator Competence as a Maintenance Strategy
Heavy equipment operator training works because it shifts control over wear, fuel, and safety to the person who sits in the cab for 2,000 hours a year. Certification sets the standard, machine-based practice builds the skill, the daily inspection catches faults while they are cheap, and coached habits flatten every wear curve. Break any link in that chain, and the bill arrives as extra fuel, early parts, and lost machine days.
African contractors should treat the operator as the first technician and the training record as a maintenance asset. Demand a recognised heavy equipment operator certification and an OEM tier, give operators written authority to tag out defective machines, and publish construction site equipment safety rules at induction so equipment operator safety starts on day one. Fleets that run this system spend less on fuel and undercarriage, record fewer incidents, and keep certified operators longer than rivals that train once and move on.
The first move costs almost nothing. Print the excavator checklist, assign a supervisor to sign it every shift, and track fuel per engine hour for one month. Those numbers will make the case for the other six steps.
Keep Heavy Equipment Safe, Efficient, and Reliable
Explore Construction Frontier’s Equipment Ownership & Maintenance coverage for practical insights on operator training, preventive maintenance, fuel efficiency, and equipment performance. Discover proven ways to reduce breakdowns, extend machine life, and control operating costs.